
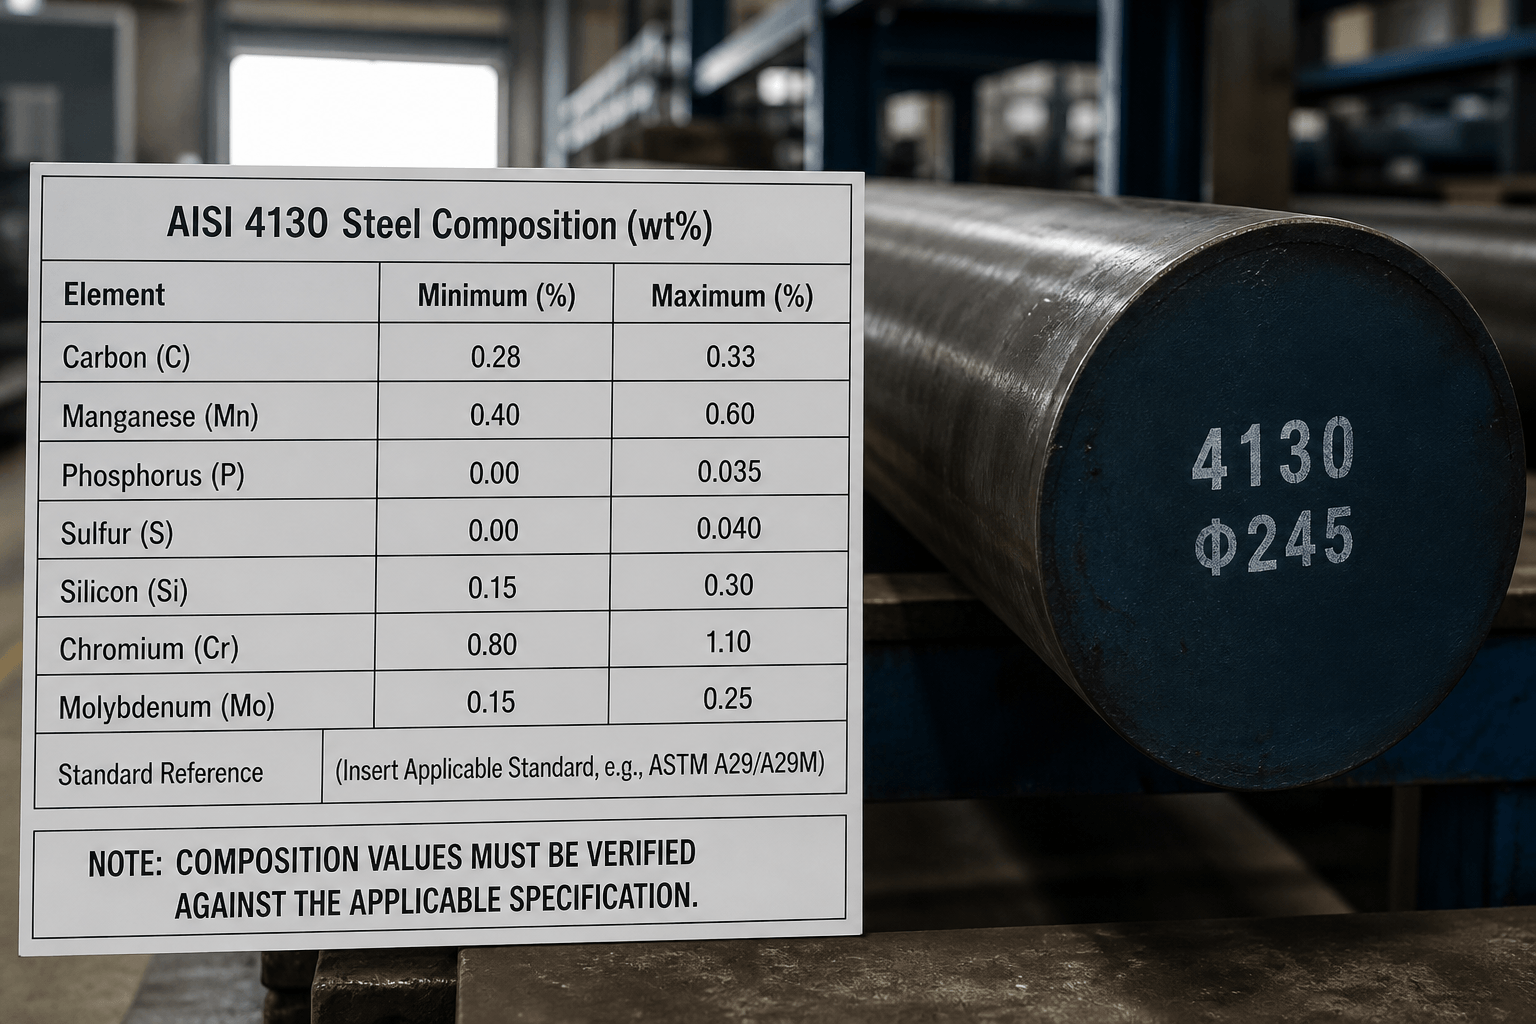
4130 steel composition describes a low-alloy chromium-molybdenum steel grade. The 4130 designation identifies a grade family, but it does not by itself provide every requirement needed to accept material. Exact chemistry limits must be read from the named material standard or purchasing specification that applies to the product form, size, and delivery condition.
A composition chart also does not guarantee a particular strength, hardness, toughness, weld result, dimensional condition, or finished-part performance. Those outcomes depend on the applicable specification, product form, processing history, heat treatment, and inspection requirements. For that reason, a buyer should compare the supplied material certificate with the same grade and product specification stated on the drawing or purchase order.
What the 4130 Designation Identifies
4130 is commonly used to identify a low-alloy steel containing chromium and molybdenum as principal alloying additions. Carbon, manganese, silicon, sulfur, phosphorus, and iron balance the chemistry within the limits established by the applicable specification. The designation is therefore a useful starting point for material selection, but it is not a complete substitute for a standard reference.
The required reference may be an applicable AISI, SAE, ASTM, or other material specification, depending on the product form and purchasing requirement. A 4130 tube, bar, sheet, plate, forging, or other product may be governed by different requirements. The product form, size or thickness, heat-treatment condition, and testing or certification requirements should be stated separately from the grade name.
| Item | What it tells the buyer |
|---|---|
| Grade designation | The intended alloy family, such as 4130. |
| Material specification | The document that defines applicable chemistry, product, testing, and delivery requirements. |
| Product form | Whether the material is supplied as tube, bar, sheet, plate, forging, or another form. |
| Material condition | The supplied condition, processing history, or heat-treatment state required by the specification. |
| Acceptance criteria | The evidence required for chemistry, dimensions, appearance, mechanical properties, or other requirements. |
How to Read a 4130 Steel Composition Chart
A 4130 composition chart should be read as a specification-controlled chemistry table, not as a general-purpose list of typical values. Before reviewing the element rows, identify the standard or purchasing specification printed beside the table. Confirm that it applies to the supplied product form and size.
| Chart field | How to interpret it | What to verify |
|---|---|---|
| Element name | Identifies the chemical constituent being controlled. | Use the same element names and notation as the applicable specification. |
| Minimum limit | Sets a lower permitted value when the specification uses a minimum. | Check whether the limit applies to the grade, product form, and stated condition. |
| Maximum limit | Sets an upper permitted value when the specification uses a maximum. | Confirm that the certificate result does not exceed the applicable limit. |
| Balance or remainder | Indicates that iron and permitted constituents make up the remaining chemistry. | Do not treat “balance” as an unrestricted acceptance statement; use the complete specification. |
| Specification reference | Defines which limits and test requirements govern the table. | Match the reference on the chart, order, certificate, and inspection plan. |
Minimum and maximum values have different meanings. A minimum is a lower boundary, while a maximum is an upper boundary. Some specifications may also control residual elements, reporting rules, product analysis, or permitted variations. A certificate result should therefore be evaluated against the exact acceptance criteria rather than against an informal online chart.
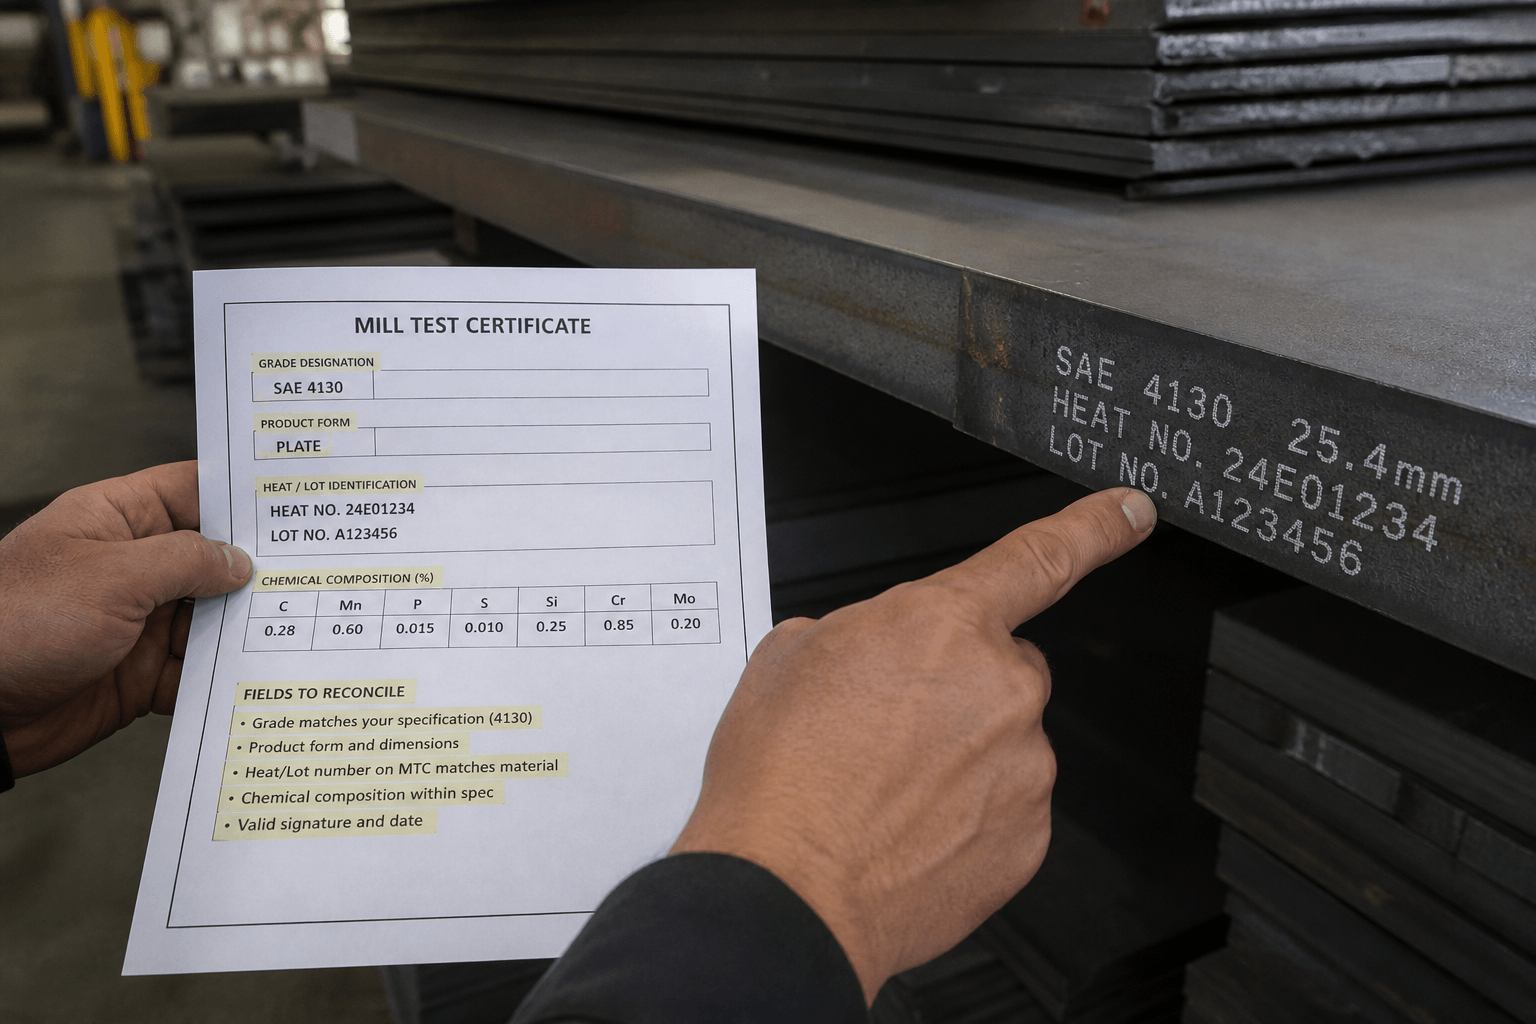
The certificate should show the grade designation, applicable specification, product form, heat or lot identification, and reported chemistry results when those documents are required by the order. The heat or lot number provides the link between the certificate and the material received. If the grade, product form, specification, or identification does not match the purchase documents, the chemistry result should not be treated as sufficient proof of compliance.
Why the Principal Elements Matter
The elements in 4130 are relevant because they influence how the steel responds to processing and service. Their effects should be described as material-selection considerations, not as guaranteed properties from chemistry alone.
| Element or group | General relevance | Important qualification |
|---|---|---|
| Chromium | Can contribute to hardenability and the response of the alloy to heat treatment. | The resulting properties depend on chemistry, section size, thermal cycle, and condition. |
| Molybdenum | Can support hardenability and strength potential in a low-alloy steel system. | It does not establish a finished-part property without the required processing and tests. |
| Carbon | Contributes to strength potential and affects processing and joining considerations. | The result must be evaluated with the complete chemistry and material condition. |
| Manganese | Can influence hardenability and strength, while also forming part of the controlled steel chemistry. | Its effect is not independent of the other alloying elements or process history. |
| Silicon | Can support deoxidation and influence the steel’s response to processing. | Acceptance remains governed by the applicable specification. |
| Sulfur and phosphorus | Are controlled constituents that can affect material behavior and processing when present within the permitted range. | Do not infer weldability, toughness, or machinability from one reported value alone. |
| Iron | Forms the balance of the steel matrix. | “Balance iron” does not replace the requirement to review all controlled elements. |
Composition can indicate the intended alloy family and help explain its response to treatment, but it cannot replace mechanical testing, dimensional inspection, surface inspection, weld inspection, or assembly checks. A composition certificate confirms a chemistry claim within the stated acceptance system. It does not by itself confirm that a finished component meets every drawing requirement.
4130 Compared With 4140 and 1018
4130, 4140, and 1018 are not interchangeable labels. Their chemistry families and common material-selection roles differ, but any comparison must use compatible specifications and the same product-form and condition assumptions. The table below is intentionally qualitative because exact limits must come from the applicable specifications.
| Grade | High-level composition distinction | What the designation does not establish |
|---|---|---|
| 4130 | A chromium-molybdenum low-alloy steel grade with controlled carbon and other constituents. | It does not establish a finished strength, hardness, weld result, or dimensional capability. |
| 4140 | A different chromium-molybdenum steel grade with its own specified chemistry limits and product requirements. | It should not be substituted for 4130 based only on the shared chromium-molybdenum description. |
| 1018 | A plain-carbon steel grade family rather than the same low-alloy chromium-molybdenum system. | Its comparison with 4130 still requires a defined product form, condition, property, and application requirement. |
“Stronger” is not a complete comparison. The question must identify the property, test basis, product form, and material condition. Heat treatment, section size, processing history, and specification requirements can change the comparison. Similarly, a statement about toughness, weldability, machinability, or suitability needs a defined condition and supporting technical basis. Chromoly does not automatically mean that one supplied part will outperform every other steel in every application.
For machined components, the verified material requirement must carry into the part drawing, process plan, and inspection records. Custom CNC machining from first sample to repeat production may be relevant when the approved 4130 material is used for a machined part, but machining does not replace material verification. For transportation-related OEM work, custom metal fabrication for automotive and transportation equipment should likewise be considered separately from the chemistry acceptance decision.
What to Verify Before Accepting 4130 Material
A buyer or OEM should define the material evidence before placing the order. The sequence below keeps chemistry verification separate from other acceptance activities:
- Identify the grade and specification. State 4130 together with the applicable material standard or purchasing specification. Do not rely on the grade number alone.
- Define the product form and size. Record whether the requirement is for tube, bar, sheet, plate, forging, or another form, along with the relevant thickness, diameter, or dimensions.
- Define the material condition. State any required delivery or heat-treatment condition in the governing documents. Do not infer condition from the grade designation.
- Require traceable documentation. Specify whether a material test report or certificate is required, and require the grade, specification, heat or lot number, product form, and chemistry results to be traceable to the shipment.
- Compare chemistry with the correct limits. Review each reported result against the same specification and product requirements named in the order.
- Inspect other requirements separately. Dimensional fit, visual condition, mechanical properties, weld quality, surface finish, and assembly performance require their own criteria and records where applicable.
This process is especially important when a prototype will become repeat production. The material certificate should identify what was supplied, while the drawing and inspection plan should identify what the completed part must achieve. Those are related records, but they answer different questions.
Where RFQ Assumptions Create Cost and Production Risk
Many sheet metal fabrication problems begin before production starts. If drawings, tolerances, finish expectations, material grades, or assembly requirements are unclear, suppliers may quote based on different assumptions. That can make prices difficult to compare and may lead to rework, cosmetic rejection, assembly misalignment, or production delays later.
For OEM buyers, the goal is not simply to request the lowest price. The goal is to make sure each supplier is quoting the same manufacturing reality. Before confirming an order, clarify which dimensions are fit-critical, which surfaces are cosmetic, whether prototypes must match batch-production conditions, and how finished parts will be inspected.
Frequently Asked Questions
What 4130 steel composition details should buyers define before requesting a quote?
Buyers should define the functional requirement, drawing notes, critical dimensions, material or process expectations, and any inspection points related to 4130 steel composition. This helps suppliers quote the same manufacturing scope instead of making different assumptions.
How can RFQ details affect cost, fit, or lead time?
RFQ details can change tooling, forming, welding, finishing, inspection, or rework requirements. If buyers do not clarify it early, two supplier quotes may look comparable while covering different production risks.
Why should drawing requirements be reviewed before prototype approval?
drawing requirements may look acceptable on a single sample but become harder to control during batch production. Buyers should confirm whether the prototype reflects the same process, finish, and inspection conditions expected for production.
What inspection points matter most for 4130 steel composition projects?
Important inspection points usually include fit-critical dimensions, holes or mating areas, cosmetic surfaces, finish build-up, welded or formed features, and any dimensions that affect downstream assembly. These points should appear in the RFQ or drawing notes.
How can buyers reduce prototype approval risk before batch production?
Buyers can reduce risk by clarifying drawings, locking key material and finish assumptions, defining inspection timing, approving a representative sample, and confirming which dimensions or surfaces require tighter process control.
How can Yishang help review 4130 steel composition requirements?
Yishang can review drawings, RFQ notes, material requirements, tolerance expectations, finish details, samples, and assembly needs to identify unclear assumptions before quoting or batch production.