
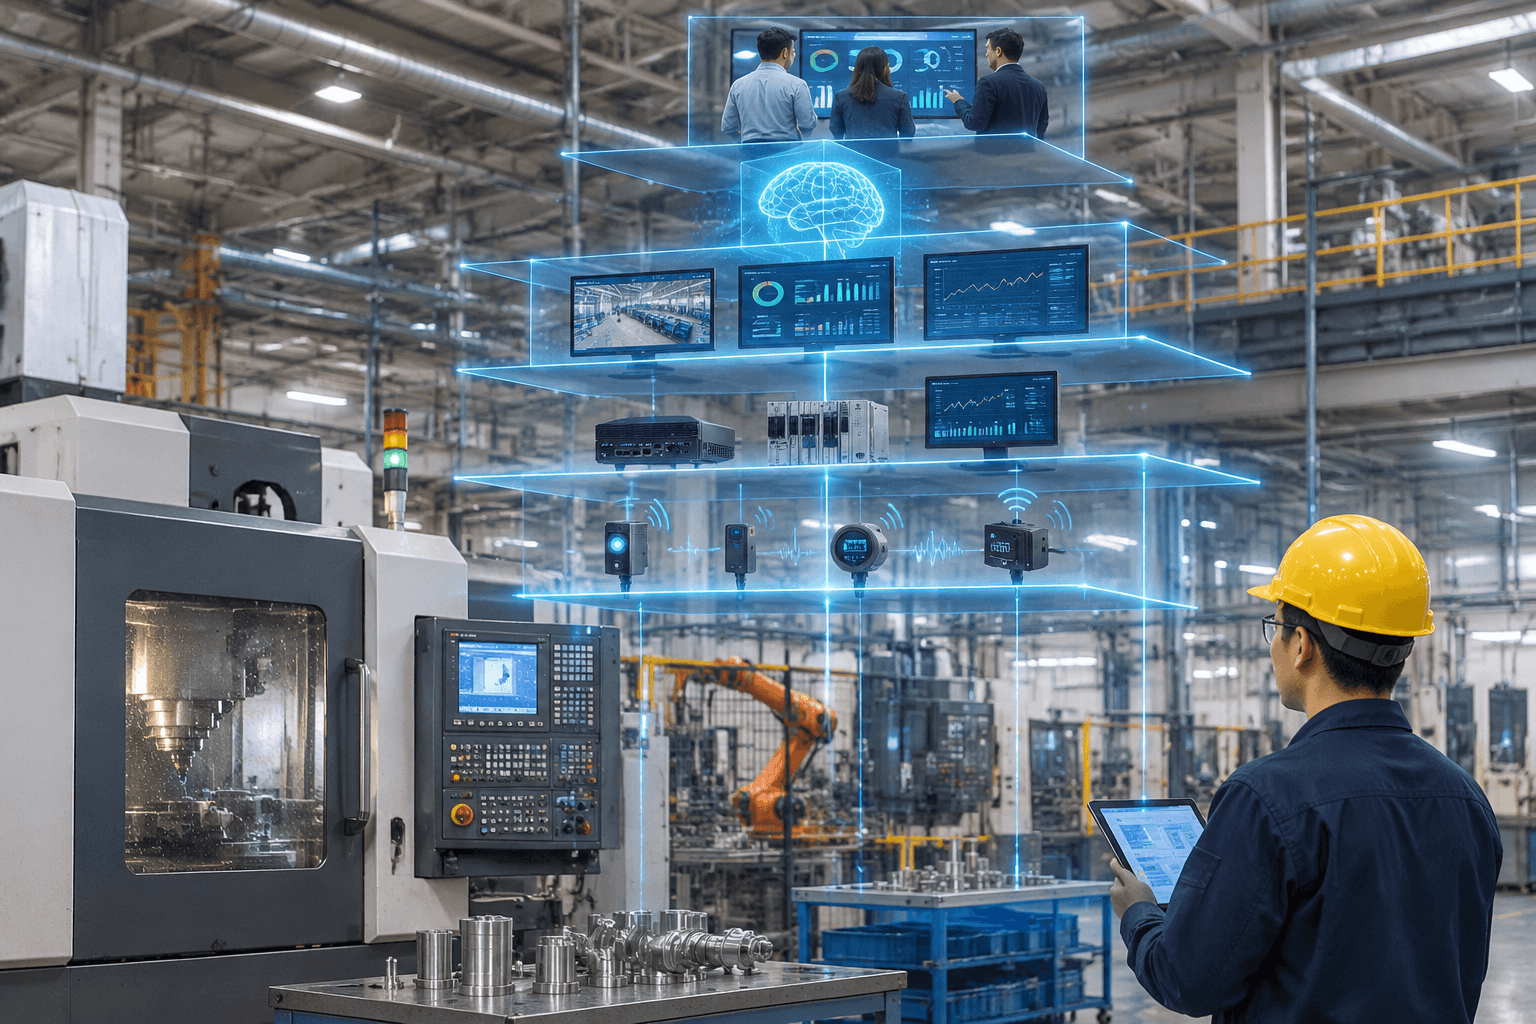
AI in Industry 4.0 is not the same as Industry 4.0 itself. Industry 4.0 creates a connected operational environment in which machines, sensors, software, production records, and people can exchange useful information. AI uses that environment’s data to explain patterns, forecast outcomes, assist decisions, or support governed autonomous action.
The practical sequence matters. A manufacturer normally needs reliable connectivity and process visibility before it can explain losses, make dependable predictions, or automate decisions. Not every plant needs to reach autonomy. The appropriate target depends on the decision being improved, the consequences of an error, the available data, and the organization’s ability to validate and govern the system.
What AI Means Within Industry 4.0
Industry 4.0 is the broader transformation of industrial operations through connected equipment, digital information flows, integrated systems, and data-supported processes. AI is one set of capabilities that can operate within this environment.
Fixed automation follows programmed logic. A controller might stop a machine when a measured value crosses a defined limit or route a part according to a preset sequence. This behavior is predictable and does not learn from historical examples.
Artificial intelligence is a broad category of systems designed to perform tasks associated with recognition, reasoning, prediction, recommendation, or decision support. Machine learning is a subset of AI that identifies patterns from data rather than relying only on manually written rules. Generative AI produces or transforms content such as text, summaries, instructions, or software queries based on a user request and the information made available to it.
These approaches are complementary rather than interchangeable. Fixed rules remain appropriate when operating boundaries are known and stable. Machine learning may help when relationships are too variable for simple thresholds. Generative AI can improve access to procedures and operational knowledge, but it should not directly control equipment without governed integration, validated logic, permissions, and safeguards.
How Industrial AI Capabilities Progress
The following maturity sequence connects each capability to its prerequisites and limits. Plants can stop at the stage that delivers sufficient operational value; controlled autonomy is not a universal requirement.
| Stage | Plant capability | Required foundation | Typical output | Main limitation |
|---|---|---|---|---|
| 1. Disconnected operations | Machines and departments operate with isolated records or manual observations. | Defined process objectives and agreement on which decisions need better information. | Manual reports, operator knowledge, and local machine readings. | Events cannot be compared reliably across equipment, products, or time. |
| 2. Connectivity | Relevant machine, sensor, production, and quality data can be collected and timestamped. | Interfaces, edge devices, network access, consistent identifiers, and suitable sensor coverage. | Data streams and event histories. | Connected data may still lack context or contain gaps and inconsistent meanings. |
| 3. Visibility | Teams can see current conditions and compare performance across defined dimensions. | Context linking measurements to equipment, jobs, products, shifts, and process states. | Dashboards, alarms, traceability records, and production status. | Visibility shows what happened but may not explain why. |
| 4. Explanation | Data analysis helps identify relationships among process conditions and outcomes. | Reliable labels, aligned timestamps, process knowledge, and enough history to compare operating states. | Probable drivers, recurring loss patterns, and anomaly classifications. | Correlation alone does not establish a controllable cause. |
| 5. Prediction | Models estimate a future condition, quality risk, demand level, delay, or process outcome. | Representative historical data and validation across relevant production conditions. | Forecasts, risk scores, anomaly warnings, and estimated outcomes. | Performance can deteriorate when products, equipment, materials, or operating conditions change. |
| 6. Decision support | AI outputs are connected to a defined human workflow. | Decision owners, action thresholds, escalation rules, audit records, and feedback on results. | Recommended inspections, schedule changes, parameter reviews, or maintenance actions. | A technically accurate prediction creates little value if nobody owns the response. |
| 7. Controlled autonomy | A validated system can take a bounded action under specified conditions. | Safe operating limits, deterministic controls, permissions, monitoring, override mechanisms, and fallback behavior. | Automatic adjustments or routing within an approved operating envelope. | Autonomy is unsuitable when consequences are poorly understood or safeguards are insufficient. |
The progression is not purely technical. Moving from prediction to action requires operational ownership. The organization must decide who receives an output, what evidence is needed before acting, which actions are permitted, and when the issue must be escalated.
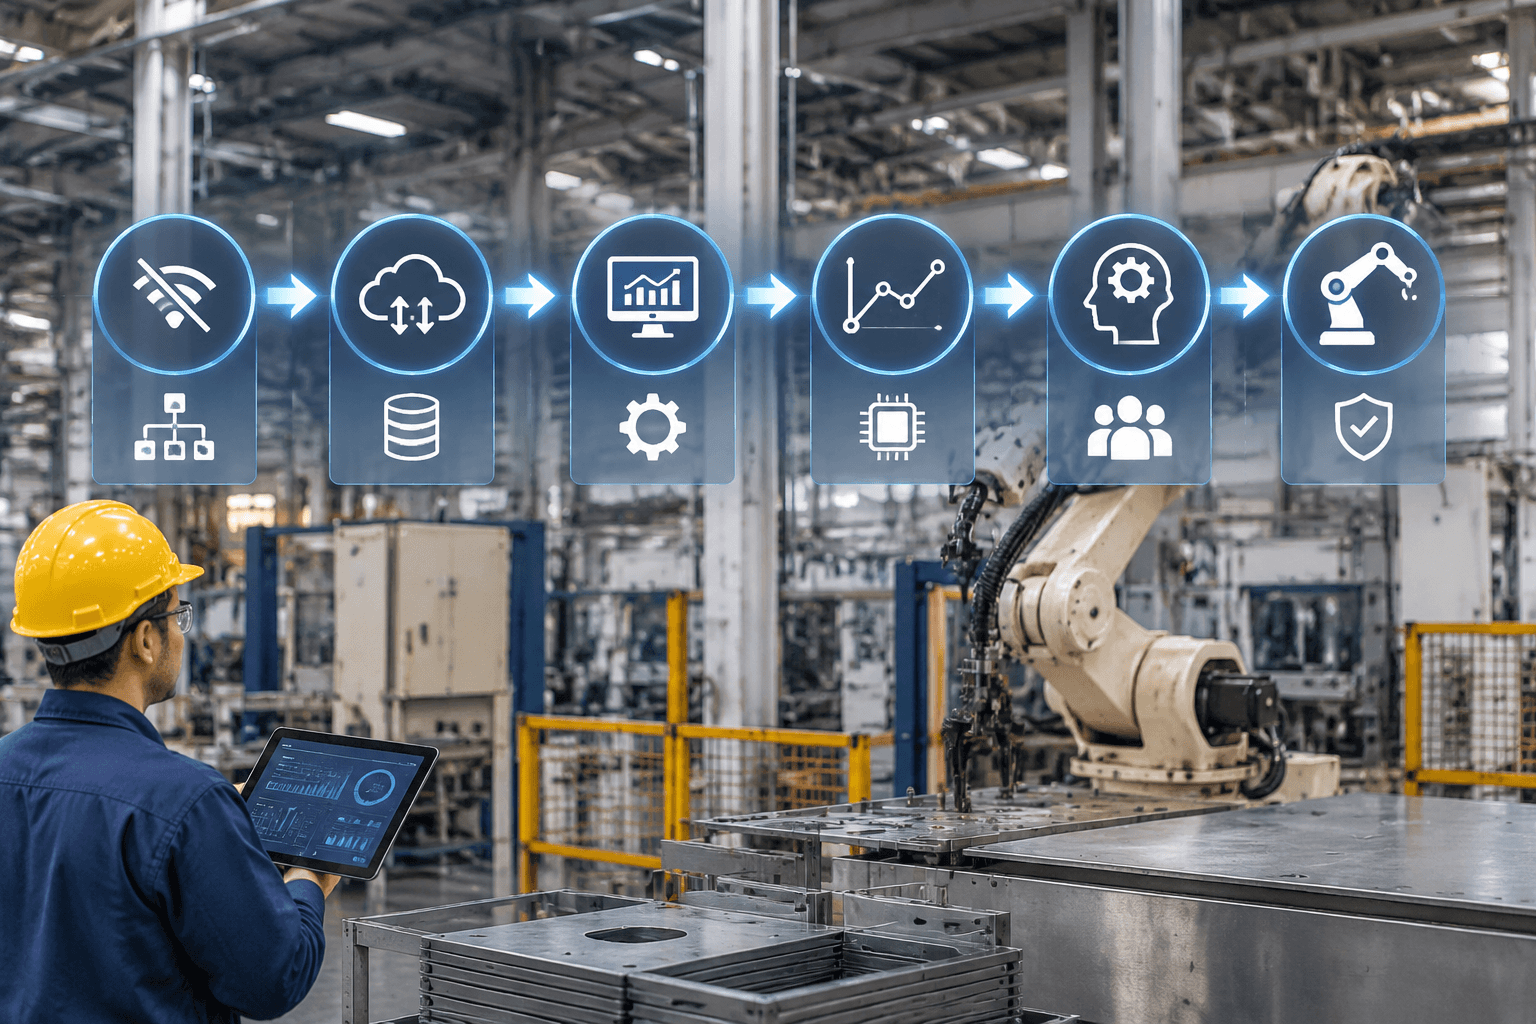
The Data and Integration Foundation
Industrial AI depends on data that represents the decision being made. Collecting every available machine tag is not the same as creating a useful dataset. Teams must identify which physical conditions, production events, and outcomes are relevant to the question.
Potential inputs include machine states, cycle events, process settings, sensor measurements, tool or consumable information, inspection results, maintenance records, work orders, product identifiers, material batches, production schedules, and operator-recorded events. The required combination changes by process and decision.
For example, visual inspection data and lighting conditions may be central to an inspection model. A scheduling model may instead require order priorities, routing, equipment availability, changeover constraints, and work-in-progress status. Welding, finishing, assembly, machining, and sheet metal fabrication therefore should not be treated as if they create identical data or require identical AI models.
Data requirements that affect reliability
- Sensor coverage: Measurements must represent the conditions associated with the target outcome, not merely what is easy to collect.
- Sampling relevance: Collection frequency should match the speed of the event. Excessive aggregation can hide short process changes, while unnecessarily frequent sampling can add volume without useful information.
- Labels: Models need trustworthy definitions of outcomes such as accepted, rejected, delayed, interrupted, or reworked.
- Context: Records should identify the applicable machine, product, job, material, tool, shift, and process state where relevant.
- Time alignment: Machine events, quality records, and production transactions need compatible timestamps so causes are not paired with the wrong outcomes.
- Historical depth: Data should include the range of conditions in which the model is expected to operate, including uncommon but important states.
- Data quality: Missing values, changed sensor definitions, duplicate events, manual-entry inconsistencies, and measurement drift must be identified rather than silently treated as normal observations.
A practical Industry 4.0 architecture
Physical process and equipment → sensors, controllers, machine interfaces, and operator inputs
Edge layer → local collection, protocol translation, filtering, buffering, rules, and time-sensitive inference
Operational systems → MES, quality, maintenance, traceability, production planning, and related applications
Data and AI layer → contextualized history, model training, validation, deployment, and monitoring
Business applications and people → decisions, approvals, actions, escalation, and outcome feedback
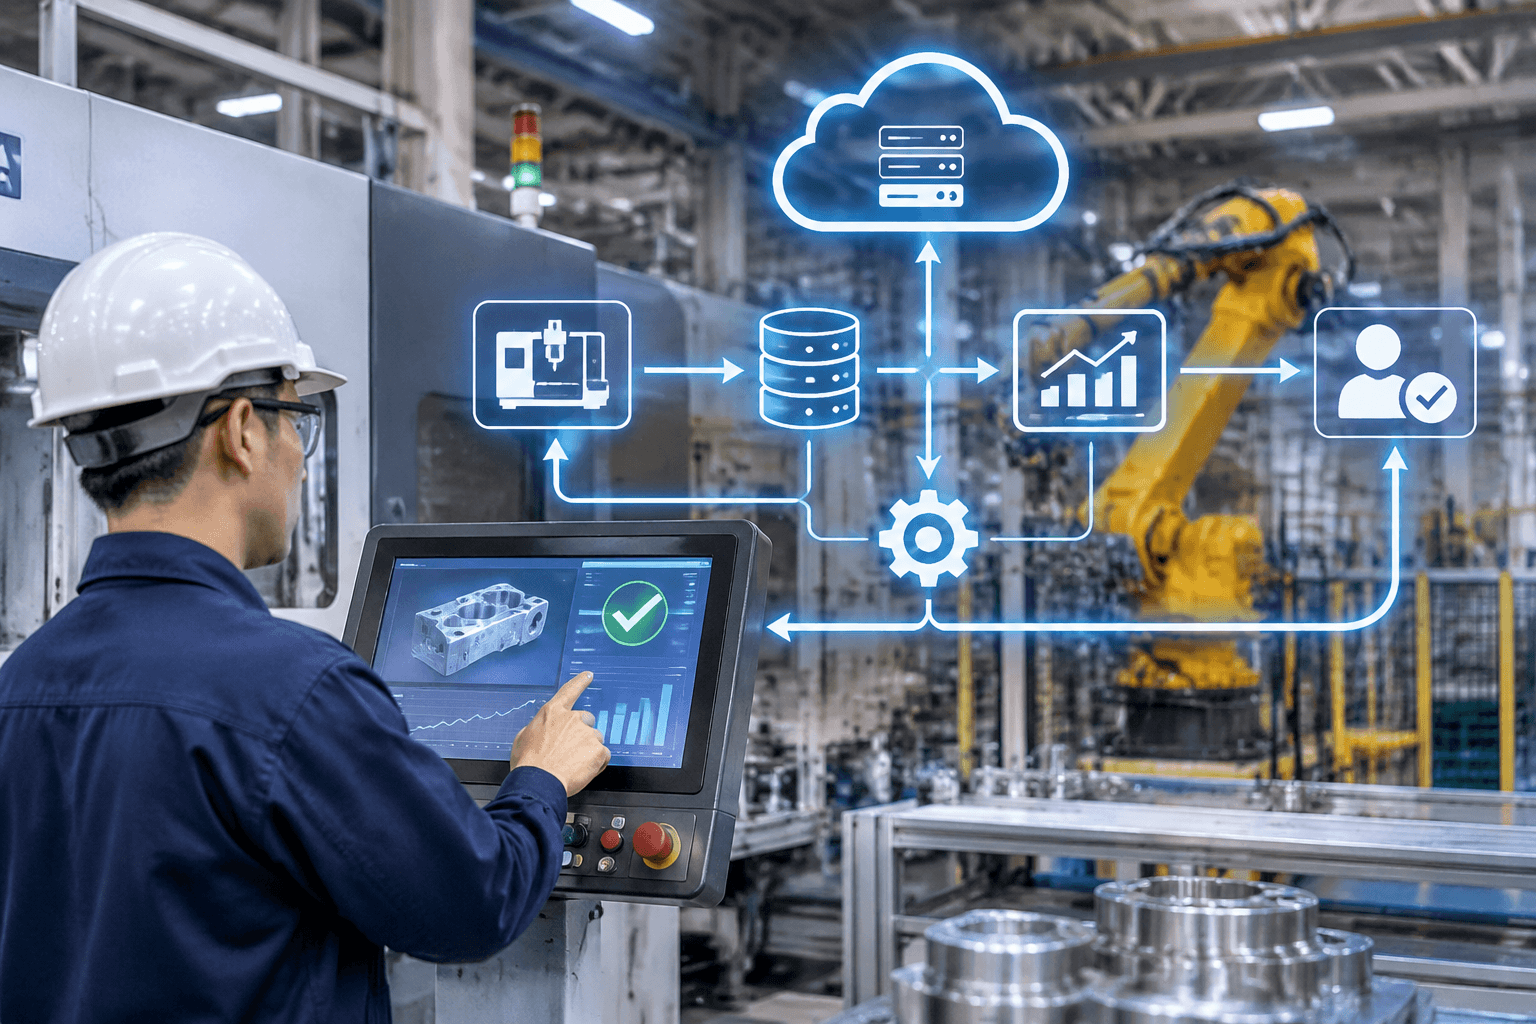
Integration should support a closed information loop. Equipment data gains meaning from production and quality context; AI outputs become operational only when they reach the appropriate application or person; completed actions and actual outcomes then return as feedback.
Where Different AI Approaches Fit
The best method is determined by the decision, not by a preference for a particular technology. A transparent rule is often better than a model when limits are stable and explainable.
| Decision or task | Suitable approach | Example use | Key requirement |
|---|---|---|---|
| Monitor a known operating boundary | Fixed rules and statistical limits | Notify an owner when a defined measurement leaves its approved range. | Stable limits and dependable measurements. |
| Identify unusual multivariable behavior | Machine-learning anomaly detection | Flag a combination of signals that differs from established operating patterns. | Representative normal data and a process for reviewing false alarms. |
| Estimate a future outcome | Forecasting or supervised machine learning | Estimate completion risk, quality risk, demand, energy use, or a future equipment condition. | Reliable outcomes, relevant predictors, and validation under actual production conditions. |
| Evaluate images | Computer vision | Support inspection of a specifically defined feature, surface, or assembly condition. | Controlled image acquisition and labeled examples reflecting acceptable variation. |
| Retrieve and summarize operational knowledge | Generative AI with governed information access | Help personnel locate procedures, summarize records, or draft a response for human review. | Approved source material, access controls, traceability, and verification. |
| Compare scheduling options | Optimization, simulation, rules, or predictive models | Evaluate possible sequences using capacity, priority, material, and changeover constraints. | Accurate constraints and an owner who can approve or reject the recommendation. |
| Adjust a process automatically | Governed control combining validated models and deterministic safeguards | Make a bounded adjustment only within an approved operating envelope. | Low-latency integration, safety controls, monitoring, fallback logic, and human override. |
Connected manufacturing environments also differ by application. In automotive and transportation equipment fabrication, traceability, production coordination, and inspection records may support separate decisions rather than one general AI model. For material handling and logistics equipment, operational and production data may similarly inform planning, quality, or logistics decisions according to the specific workflow.
Deployment Reliability and Accountability
An AI pilot can appear successful in a limited dataset and still fail during routine production. A model may have seen only one shift, product family, operator pattern, material source, machine condition, or environmental range. It can then interpret legitimate variation as an abnormal event or miss a condition absent from its training data.
Validation should separate development data from evaluation data and test performance across the conditions in which the system will be used. Relevant dimensions may include shifts, products, machines, equipment states, operators, materials, process settings, maintenance conditions, and environmental changes. The test plan should also examine missed events, false alarms, uncertain outputs, and the operational consequences of each error type.
Failure mode: an accurate model with no action workflow
A warning is not an operational result. Each output needs an owner, a response window, an allowed action, an escalation route, and a method for recording what happened.
Failure mode: operating conditions change
New products, revised settings, replaced sensors, equipment wear, maintenance work, or altered materials can shift the relationship between inputs and outcomes. Monitoring must detect when model assumptions no longer represent production.
Failure mode: automation exceeds the validated boundary
A recommendation model should not become a control system merely by connecting its output to equipment. Automated action requires separate validation, permissions, constraints, fallback behavior, and override controls.
Edge versus cloud deployment
Edge deployment places collection or inference close to the equipment. It can be appropriate when response time is short, connectivity is intermittent, data volume is high, or information should remain within the facility. The tradeoff is that many distributed devices can increase deployment, version-control, maintenance, and monitoring work.
Cloud or centralized deployment can simplify shared storage, model training, fleet-level comparison, and scaling across sites. It depends more heavily on connectivity, data-transfer arrangements, access governance, and acceptable latency.
Many architectures use both: edge systems collect and buffer data or execute time-sensitive inference, while centralized systems support historical analysis, model development, governance, and broader business integration.
What Your Plant Can Realistically Do at Each Stage
| Current condition | Realistic capability | Priority gap to close | Next step |
|---|---|---|---|
| Important records are manual or isolated. | Define the decision and create a consistent baseline. | Process-understanding and data-collection gaps. | Identify the outcome, relevant events, owners, and minimum measurements. |
| Machines are connected, but data lacks production context. | Basic monitoring and event history. | Integration and identifier gaps. | Link measurements to jobs, products, timestamps, and machine states. |
| Dashboards exist, but causes remain unclear. | Structured analysis and explanation. | Labeling, quality, and process-knowledge gaps. | Connect process conditions to verified production and quality outcomes. |
| Historical relationships are stable and representative. | Limited forecasting, classification, or anomaly detection. | Validation and monitoring gaps. | Test a bounded use case across shifts, products, and equipment states. |
| Models are validated, but responses vary by person or department. | AI-supported decisions. | Ownership and workflow gaps. | Define thresholds, responsibilities, escalation rules, and feedback records. |
| Decision workflows and operating boundaries are mature. | Controlled automation for selected low-ambiguity actions. | Safeguard and lifecycle-governance gaps. | Validate permissions, fallback behavior, overrides, and ongoing model monitoring. |
A useful readiness discussion begins with three questions: What production conditions can the team currently see? Which machine and business systems already contain relevant information? What specific decision should become faster, more consistent, or better informed? Answering these questions helps define a realistic data and integration starting point without treating AI as an all-or-nothing transformation.
Ready to Review This RFQ Before Production?
If your project involves ai in industry 4.0, send Yishang your drawings, material requirements, quantities, tolerance notes, finish expectations, photos, samples, and assembly needs through custom sheet metal fabrication support. A clearer review before quoting can reduce avoidable clarification rounds, rework, and production uncertainty.
Frequently Asked Questions
What ai in industry 4.0 details should buyers define before requesting a quote?
Buyers should define the functional requirement, drawing notes, critical dimensions, material or process expectations, and any inspection points related to ai in industry 4.0. This helps suppliers quote the same manufacturing scope instead of making different assumptions.
How can RFQ details affect cost, fit, or lead time?
RFQ details can change tooling, forming, welding, finishing, inspection, or rework requirements. If buyers do not clarify it early, two supplier quotes may look comparable while covering different production risks.
Why should drawing requirements be reviewed before prototype approval?
drawing requirements may look acceptable on a single sample but become harder to control during batch production. Buyers should confirm whether the prototype reflects the same process, finish, and inspection conditions expected for production.
What inspection points matter most for ai in industry 4.0 projects?
Important inspection points usually include fit-critical dimensions, holes or mating areas, cosmetic surfaces, finish build-up, welded or formed features, and any dimensions that affect downstream assembly. These points should appear in the RFQ or drawing notes.
How can buyers reduce prototype approval risk before batch production?
Buyers can reduce risk by clarifying drawings, locking key material and finish assumptions, defining inspection timing, approving a representative sample, and confirming which dimensions or surfaces require tighter process control.
How can Yishang help review ai in industry 4.0 requirements?
Yishang can review drawings, RFQ notes, material requirements, tolerance expectations, finish details, samples, and assembly needs to identify unclear assumptions before quoting or batch production.